At a plant I visited, the maintenance metrics looked solid. Schedule compliance was high, and maintenance management seemed confident on the surface. But the plant and production managers were not so confident.
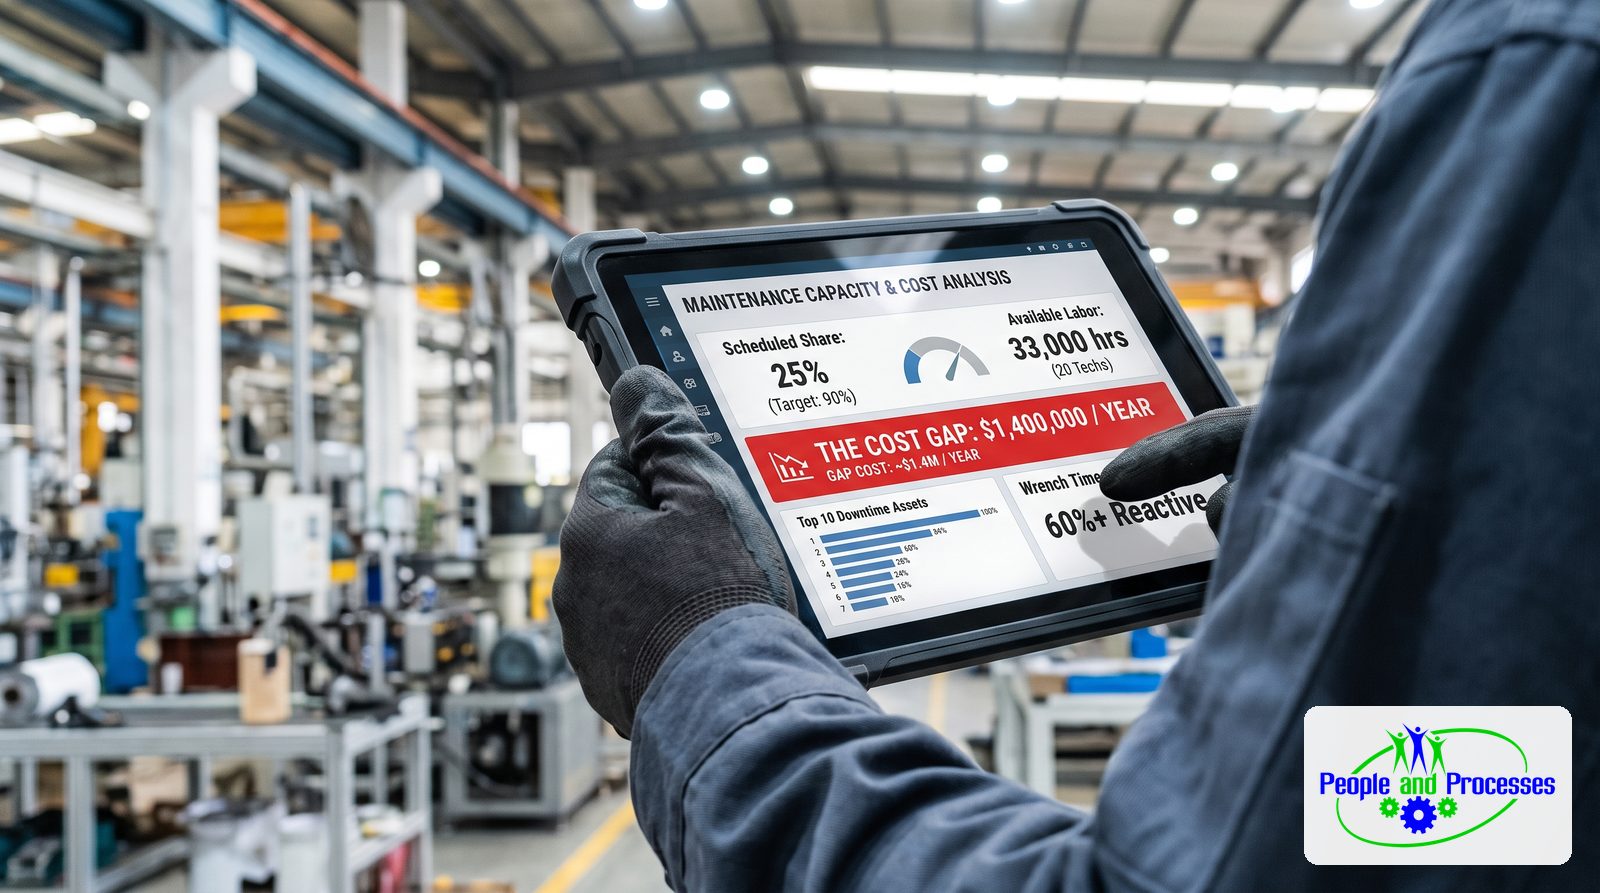
Digging deeper, I looked at the maintenance schedule. Only about 25% of available labor was scheduled; mostly PM days. Nearly everything else the crew did was reactive.
That's the trap in schedule compliance. You can hit 100% compliance when only a quarter of your labor is on the schedule. Meanwhile, unplanned work can eat 60% or more of the hours you pay for.
If you're building next year's budget right now, you might be considering asking for more technicians. Headcount is never easy to gain, so before you ask, find the capacity you're already losing.
Why your headcount request gets denied
Your plant manager decides on cost and risk, not on equipment availability percentages or schedule compliance numbers. Requesting two more technicians is a cost increase with no proof it changes the outcome.
In a reactive plant, it usually doesn't. More people in a reactive plant fight more fires. The new hires get absorbed into breakdowns the same way your current crew did. It's the vicious cycle of doom.
Some plants do need more technicians. But you can't prove it, or keep new hires productive, until you know how much of your current labor is planned.
The cycle that keeps your schedule small
Unplanned downtime drives everything. When equipment fails, production loses output, so production protects its equipment from maintenance too. They've learned that when they give you access, one of two things happens: the job runs past the time you promised, or the equipment fails at startup because the work wasn't done right.
Maybe you get PM days and not much else. The work that would prevent the next failure never makes it onto the schedule. The planner gets pulled into sourcing emergency parts because no one with authority has said that has a cost. Detailed corrective job plans and PMs that address the likely failure modes never get built, and the cycle repeats.
The conditions that keep this cycle going were set at the maintenance manager level and above. Breaking it starts with planned work that production can trust.
Every downtime event shrinks the schedule. Every planned job that finishes on time and starts up reliably earns access for the next one.
Run your own numbers before the meeting
Pull three numbers from your CMMS. Do it as you read this, not the night before the meeting.
1. Your scheduled share. Take the labor hours entered in the weekly schedule this year and divide them by your available paid labor hours. In a well-run operation, that's 90% or more. In many plants, it's under 60%, sometimes far less. If your compliance is high and this number is low, you've found the utilization trap.
2. Your top downtime assets. List the 10 bad-actor assets with the most downtime over the last 30 days. You can bet that your plant and production managers know them. Each downtime event is profit lost forever. These assets are where the reactive cycle starts, and where your first detailed job plans should go.
3. What the gap costs, in dollars and in people. Start with the cost of an hour: pay plus benefits, divided by the hours you pay for in a year. Employer costs typically add about 35% to salary, ranging from about 15% to 65% or more. Then multiply your available hours by the difference between 90% and your share, and by the cost of an hour.
Here's an illustration for a 20-person crew scheduling 25% of its labor:
| Step | Example |
|---|---|
| Available labor hours | 20 technicians × 1,650 hours = 33,000 hours |
| Gap to 90% | 90% − 25% = 65% |
| Hours not planned and scheduled | 33,000 × 65% = 21,450 hours |
| Cost of an hour | $100,000 + 35% = $135,000 ÷ 2,080 paid hours ≈ $65 |
| Cost of the gap | 21,450 × $65 ≈ $1.4 million a year |
Available hours are what's left of 2,080 paid hours after vacation (80), holidays (72), sick and personal time (40), two 15-minute breaks and a 20-minute morning meeting each workday (about 197 over 236 workdays), and training and safety time (40). Use your own figures.
That cost rarely shows up as a single line item in the budget. Those hours still go to reactive jobs that take longer than they should, so you won't recover all of it. Plants that consistently perform their planning function recover 30% to 50% of maintenance labor capacity. For a 20-person crew, that's the capacity of 6 to 10 technicians. Compare that with the two you were going to ask for.
The test your plant manager may give you
When I work with plant managers, I tell them to walk into the maintenance manager's office and ask two questions:
- Can you show me three detailed corrective job plans developed this week?
- Can you show me next week's schedule with labor hours for each day versus the anticipated paid hours?
I don't mean a work order. I mean a reusable job plan with craft hours, a parts list, and step-by-step, precise task instructions a new technician can follow.
How one plant went from 25% to 70% in 18 months
The plant I started the article with didn't hire its way out. They broke the cycle by getting planned work right, starting with good preventive maintenance and planned corrective work on the assets causing the most downtime.
Each job that finished on time and started up reliably built trust with production. Production released equipment more readily. Less downtime meant less reactive work, which freed hours for the next round of planned work. As unplanned work fell, they put more on the schedule.
In 18 months, scheduled labor went from about 25% to about 70% of available hours.
The payback comes from what planning removes. On average, each hour spent on planning eliminates three to five hours of execution: the time technicians lose looking for information, chasing materials, waiting for equipment, and working on the wrong priority. Most organizations run at 25% to 35% wrench time. Best-in-class is 55% to 65%.
Other plants see the same pattern. At a packaging facility, a dedicated planner role took wrench time from 30% to 55% without additional staff, and overtime fell 20%. At a chemical plant, coaching on effective work execution returned $1.8 million to the plant budget in the first year. None of it came from a technology investment or added headcount.
What to ask for instead
Walk into the meeting asking for what breaks the cycle. Plant leadership is the only group that can give you the first three.
- Define what planning produces: detailed corrective job plans, and a weekly schedule with available labor hours for each day.
- Protect the planner's time. Only about 10% of planners are truly planning maintenance work. The rest chase parts, coordinate contractors, manage emergencies, and field production down calls.
- Plant leadership has to hold maintenance and production accountable to the schedule, including releasing equipment when promised and getting it back when promised.
- A planner trained to produce that work. If you need headcount, this is the hire that pays for itself. If you already have a planner, they and maintenance supervision need the training and coaching to deliver what you're about to promise.
Put it on one page before you go in: your ask, your planned and scheduled share, your downtime list, what the gap costs, and what planning returns.
Train and coach your planner(s) and protect their time
Our three-day Maintenance Planning and Scheduling course teaches your team to plan work that production will release equipment for:
- Detailed job plans with craft hours, parts lists, and precision task steps
- Locked schedule windows and a weekly schedule with labor hours for each day
- Supervisors, production, and planners aligned (roles and responsibilities) so the schedule actually means something
Your people leave able to answer both of your plant manager's questions.
Who should attend: planners, maintenance supervisors, and maintenance managers. Bring a production counterpart if you can.
Follow-on coaching through our Planner & Scheduler Competency Development & Coaching Program keeps the new practices in place as you add more to the schedule.
Reserve a seat in an upcoming session now and charge it to the budget you're building.